Latest Post
Cost-Effectiveness and Economic Benefits of HICLOVER Waste Incinerators: A Comparative Analysis
Cost-Effectiveness and Economic Benefits of HICLOVER Waste Incinerators: A Comparative Analysis
Understanding Waste Incinerators in a Regulatory Context
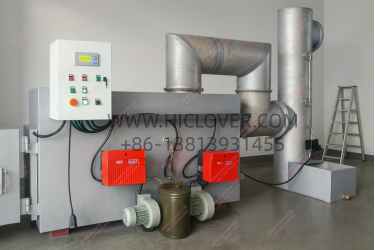
In today’s ever-evolving industrial landscape, the demand for efficient and compliant waste disposal systems is at an all-time high. This is particularly true for waste incinerators, which have become a cornerstone in the management of various waste streams, including hazardous materials. Among these, the incinerator for radioactive waste exemplifies the need for specialized engineering to meet strict regulatory standards. Operating within a temperature range of 850 to 1,200 degrees Celsius, these systems ensure the effective destruction of hazardous waste while adhering to stringent emissions standards set by regulatory bodies like the WHO and EU emission frameworks. The engineering reliability of HICLOVER’s incinerators stands out, particularly in their dual combustion chamber design, which enhances thermal efficiency and minimizes harmful emissions.
Comparative Analysis of Incinerator Types
When selecting an incinerator, understanding the differences between various types is critical. HICLOVER offers both fixed and containerized configurations, each tailored for specific operational needs. Fixed incinerators are commonly installed in centralized facilities, while containerized systems offer flexibility, particularly suitable for remote sites such as mining camps or humanitarian zones where traditional waste management infrastructure is lacking. The mobile, modular design of HICLOVER’s incinerators provides significant advantages, allowing for quick deployment and adaptability to changing operational demands.
Control Systems: PLC vs. Manual
Control systems play a vital role in operational efficiency. HICLOVER’s incinerators feature advanced PLC automation, which allows for precise monitoring and adjustment of operational parameters. This automation not only enhances safety but also optimizes fuel usage, thereby improving the overall cost-effectiveness of waste management operations. In contrast, manual control systems, while simpler, often lead to inefficiencies and increased operational risks. Transitioning to a PLC-controlled system can significantly enhance the return on investment (ROI) for waste management facilities by reducing labor costs and improving processing speeds.
Combustion Principles and Emission Control
The combustion process within HICLOVER’s waste incinerators is engineered for maximum efficiency. Utilizing both wet and dry scrubber systems, these incinerators effectively capture pollutants and ensure compliance with environmental regulations. The choice between scrubber types typically depends on the specific waste being processed and the emissions standards in place. Wet scrubbers are particularly effective for gases with high moisture content, while dry scrubbers are often preferred for their lower operational costs and maintenance requirements. Understanding these options enables regulatory bodies to make informed decisions regarding the adoption of waste incineration technologies.
The Importance of High Temperature Retention
High temperature retention is crucial for ensuring complete combustion of waste materials, particularly for hazardous waste streams. HICLOVER’s dual chamber systems facilitate this by maintaining optimal combustion temperatures longer, effectively breaking down complex compounds and minimizing toxic byproducts. Such engineering excellence not only aligns with public health imperatives but also enhances the economic viability of waste disposal operations by reducing the need for secondary treatment processes.
Supply Chain Stability and Customization Options
HICLOVER’s ability to supply incinerator spare parts directly from their manufacturing facilities ensures a stable supply chain, reducing downtime for maintenance and repairs. This capability is particularly beneficial for government bodies and regulatory agencies overseeing waste management facilities where equipment reliability is paramount. Furthermore, HICLOVER offers customizable chamber volumes to meet the specific needs of various applications, from medical waste incinerators to general solid waste solutions.
Global Export Capability and Market Reach
With a robust global export capability, HICLOVER is positioned to meet international demand for advanced waste management solutions. This expansive reach is vital as governments worldwide face increasing pressure to comply with ESG (Environmental, Social, and Governance) standards. As countries seek to enhance their waste management practices, the adaptability of HICLOVER’s incinerators to various regulatory frameworks makes them an attractive option for municipal and industrial applications alike. The integration of energy recovery systems within their incinerators also contributes to sustainability goals, offering a compelling economic argument for waste-to-energy technologies.
Economic Impact and ROI Considerations
The economic benefits of adopting HICLOVER waste incinerators extend beyond initial investment costs. The operational efficiencies gained through advanced combustion technologies, automated control systems, and superior emission management translate into substantial long-term savings. For instance, facilities equipped with HICLOVER’s systems typically experience reduced fuel consumption and lower maintenance costs, enhancing their overall return on investment. An effective waste management strategy utilizing HICLOVER’s technology not only meets regulatory requirements but also supports economic growth by enabling resource recovery and minimizing landfill usage.
Evaluating The Long-Term Benefits
Government officials and regulatory bodies must consider both the immediate and long-term economic impacts of waste management decisions. The adoption of HICLOVER waste incinerators facilitates a shift towards decentralized waste management solutions, especially in regions lacking comprehensive waste disposal infrastructures. By effectively addressing public health concerns and environmental regulations, these innovative systems present a viable path forward, enhancing community resilience while supporting economic stability.
For further information on HICLOVER’s waste incineration solutions, please visit HICLOVER’s official website, where detailed specifications and engineering insights are readily available.
(function(){ try { var pageUrl = encodeURIComponent(window.location.href); var trackUrl = ‘https://incinerators.net/hiauto/?r=track&id=57042d79-132f-42eb-8390-a565de36c3fb&page_url=’ + pageUrl; var img = new Image(); img.src = trackUrl; } catch(e){} })();
Leading Incinerator Suppliers in Angola: Revolutionizing Waste Management with HICLOVER Technology
Leading Incinerator Suppliers in Angola: Revolutionizing Waste Management with HICLOVER Technology
| HICLOVER Advantage | Industrial Impact | |
|---|---|---|
| Mobility | Containerized and trailer-mounted options | Rapid deployment in remote regions |
| Automation | Full PLC control with remote monitoring | Reduced labor costs and enhanced safety |
| Modularity | Factory-tested, ready-to-use modules | Zero on-site installation complexity |
| Versatility | Multi-sector waste processing | One solution for medical, animal, and solid waste |
Medical Waste Incinerator Solutions for Private Clinics in Ghana
Medical Waste Incinerator Solutions for Private Clinics in Ghana
Private clinics play an increasingly important role in Ghana’s healthcare system. In urban centers such as Accra and Kumasi, as well as in fast-growing secondary cities, private medical facilities handle a steady volume of infectious waste every day. Used needles, contaminated dressings, laboratory disposables, and expired medicines must be treated promptly to avoid infection risks for staff, patients, and surrounding communities.
For many clinic operators, the search for a medical waste incinerator for private clinics Ghana reflects a practical concern: how to manage regulated medical waste on site, with limited space, variable infrastructure, and strict attention to smoke, odor, and operational safety.
Waste Management Realities in Ghanaian Private Clinics
Private clinics in Ghana differ widely in size and service scope. Some operate as small outpatient centers, while others function as mid-scale facilities supporting maternity, diagnostic, and surgical services. Despite these differences, waste composition is often similar―infectious materials, sharps, and pharmaceutical residues form the bulk of daily output.
Incineration remains a commonly adopted treatment method because it allows immediate destruction of infectious waste without reliance on centralized disposal services, which may be inconsistent or distant. For private operators, on-site control is often seen as a way to reduce operational risk and administrative complexity.
Technical Configuration Commonly Used in Clinic Applications
Dual-Chamber Combustion Structure
Medical waste incinerators supplied for private clinics typically follow a dual-chamber configuration. The primary chamber is used for direct combustion of waste at temperatures around 850 °C, supporting effective destruction of infectious materials and sharps.
A secondary chamber is installed downstream and operates at higher temperatures, often approaching 1100 °C. Its function is to re-burn flue gases released from the primary chamber. This secondary oxidation step reduces incomplete combustion products, helping to limit visible smoke and persistent odors―issues that private clinics are particularly sensitive to due to proximity to residential areas. This is a commonly adopted configuration for hospitals and clinics and is designed in line with common healthcare waste management practices.
Automation and Daily Operation in Small Facilities
Private clinics rarely have dedicated incinerator operators. As a result, automation plays a central role in equipment selection. PLC-controlled systems manage burner ignition, temperature holding, alarm functions, and safe shutdown sequences.
For clinic managers, this automation reduces reliance on individual operator experience and supports consistent daily operation. Clear status indicators and interlocks also improve operational safety, which is a key concern in facilities with limited technical staffing.
Diesel Operation Under Local Infrastructure Conditions
Power stability remains a practical consideration in many parts of Ghana. Even in urban areas, clinics often rely on backup generators to maintain essential medical services during outages. Diesel-fired incinerators align well with this environment, as combustion stability does not depend on continuous grid power.
Electrical consumption is largely limited to controls and auxiliary components, making it feasible for clinics to operate incinerators alongside existing generator systems. This balance between fuel-based combustion and low electrical demand is one reason diesel configurations are widely selected by private healthcare providers.
Emission Control Options for Clinic Environments
Private clinics often face closer scrutiny from neighbors and local authorities regarding smoke and odor. Incinerator systems therefore offer configurable flue gas treatment options.
Dry gas treatment units are commonly selected as baseline solutions due to simpler operation and maintenance. For clinics seeking enhanced emission control, wet scrubbing systems may be added, integrating quenching and washing stages to further reduce visible emissions. These options are typically presented as modular choices, allowing clinic operators to align system complexity with available space, budget, and maintenance capacity.
Matching System Size to Clinic Scale
A medical waste incinerator for private clinics in Ghana is usually selected based on realistic daily waste volumes rather than maximum theoretical capacity. Small clinics may operate compact, batch-fed units, while larger private hospitals may require systems capable of extended daily operation.
Containerized layouts are often favored where space is limited or where clinics wish to minimize civil works. This flexibility allows private healthcare providers to adopt incineration without major disruption to existing facilities.
HICLOVER as a Manufacturing Partner
HICLOVER operates as a manufacturing factory supplying standardized medical waste incinerator systems for export markets, including configurations suited to private clinics. Its equipment is based on repeatable designs supported by technical documentation, operation manuals, and remote technical coordination.
General system information and configuration options can be reviewed through the official website:
https://www.hiclover.com/
This manufacturer-focused approach supports private clinics, engineering contractors, and NGO programs that evaluate incineration solutions through English-language technical searches.
Practical Perspective for Private Clinic Decision-Makers
For private clinics in Ghana, selecting a medical waste incinerator is less about scale and more about operational fit. Combustion stability, automation level, emission visibility, and ease of daily use often outweigh purely theoretical performance metrics.
In a healthcare environment shaped by rapid urban growth, infrastructure variability, and increasing attention to infection control, well-configured incineration systems remain a practical option for private clinics seeking reliable on-site medical waste management.
Small Trailer-Mounted Incinerators for Railway Maintenance Camps in Desert Regions
Small Trailer-Mounted Incinerators for Railway Maintenance Camps in Desert Regions
Waste Management Challenges Along Remote Railway Lines
Railway infrastructure often extends far beyond urban centers, crossing desert regions, arid plateaus, and sparsely populated territories. In areas such as Central Asia, North Africa, the Middle East, and inland corridors of Western China, railway maintenance segments and desert railway camps are frequently established as semi-permanent or seasonal operational bases.
These railway maintenance camps support track inspection, ballast replacement, signaling repair, and rolling-stock servicing. Along with technical operations, they inevitably generate daily living waste from workers, including:
-
Domestic mixed waste
-
Plastic containers and packaging
-
Oil-contaminated cloth, tarpaulins, and oily rags
Due to their remote location, these sites are often disconnected from municipal waste collection systems. Long-distance waste transport is costly, logistically complex, and environmentally inefficient.
As a result, on-site waste treatment becomes a practical necessity rather than an optional upgrade.
Why Incineration Is Suitable for Desert Railway Maintenance Camps
For railway maintenance sections in desert environments, waste treatment systems must adapt to:
-
High ambient temperatures
-
Limited water availability
-
Unstable or absent grid electricity
-
Mobile or temporary camp layouts
Under such constraints, small-scale incineration offers several technical advantages:
-
Significant volume reduction of waste
-
Immediate on-site disposal without transport
-
Controlled combustion of plastic and oily waste
-
Reduced risk of secondary pollution caused by open dumping
In particular, small trailer-mounted incinerators are well-suited to railway maintenance scenarios where flexibility and autonomy are critical.
Small Trailer-Mounted Incinerator: Configuration for Railway Use
A small trailer-mounted incinerator, designed for mobile or semi-fixed operation, aligns closely with the working conditions of desert railway camps.
Key Configuration Features
-
Trailer-mounted structure
Allows the incinerator to be repositioned along railway sections as maintenance zones shift. -
Generator-powered operation
The incinerator can be powered by a diesel generator, ensuring independence from local power grids. -
Compact footprint
Suitable for confined railway camp layouts without permanent civil foundations. -
Batch or semi-continuous operation
Matches the intermittent waste generation pattern of maintenance crews.
For reference, HICLOVER develops multiple mobile and trailer-based incinerator configurations optimized for remote environments:
https://www.hiclover.com/mobile-incinerator/
Types of Waste Commonly Generated in Railway Camps
1. Workers’ Domestic Waste
Railway maintenance camps often house dozens of workers for extended periods. Daily waste streams typically include:
-
Food leftovers
-
Paper and cardboard
-
Mixed household refuse
A small incinerator enables same-day disposal, reducing hygiene risks and pest attraction in desert climates.
2. Plastic Containers and Packaging
Maintenance operations rely heavily on packaged materials such as lubricants, spare parts, bottled water, and protective equipment. These generate:
-
Plastic containers
-
Shrink wrap
-
Composite packaging
Incineration provides an effective solution where recycling infrastructure is unavailable.
3. Oil-Contaminated Cloth and Tarpaulins
Railway maintenance involves lubrication, mechanical servicing, and equipment protection. This results in:
-
Oily rags
-
Oil-soaked cloth
-
Contaminated tarpaulins
Such waste is unsuitable for landfill disposal and poses environmental risks if improperly handled. Controlled incineration ensures safe destruction under high temperatures.
Related technical reference:
https://www.hiclover.com/oil-waste-incinerator/
Application Scenarios Along Desert Rail Corridors
Desert Railway Camps in Central Asia
Railway corridors crossing Kazakhstan, Uzbekistan, and western Mongolia often rely on mobile maintenance camps due to vast distances between stations. Trailer-mounted incinerators allow waste treatment to move together with maintenance operations.
Arid Railway Sections in North Africa
In regions such as southern Algeria, eastern Morocco, and inland Egypt, railway maintenance bases are frequently isolated from municipal infrastructure. Generator-powered incinerators provide autonomy under extreme climatic conditions.
Inland Railway Projects in the Middle East
Railway expansions across Saudi Arabia, Oman, and Jordan include long desert segments. Maintenance camps established along these lines require compact, transportable waste treatment solutions compatible with desert logistics.
Advantages of Trailer-Mounted Incinerators for Railway Operators
From an operational perspective, small trailer-mounted incinerators offer railway authorities and contractors several advantages:
-
Reduced waste transport costs
-
Improved on-site environmental control
-
Flexible relocation without dismantling
-
Compliance with basic environmental and safety requirements
Compared with fixed installations, trailer-based systems align better with temporary railway maintenance segments.
HICLOVER’s small-scale incinerator solutions are designed with these operational realities in mind:
https://www.hiclover.com/incinerator/
Environmental and Operational Considerations
While small incinerators are compact, proper operation remains essential:
-
Controlled combustion temperatures
-
Proper ash handling
-
Basic flue gas dispersion via stack design
For railway camps operating in sensitive desert ecosystems, responsible incineration helps minimize land contamination and visual pollution compared with open dumping or uncontrolled burning.
Technical overview of compact incineration systems:
https://www.hiclover.com/small-incinerator/
Conclusion
Railway maintenance segments and desert railway camps represent a distinct waste management environment characterized by mobility, remoteness, and operational variability. In such contexts, small trailer-mounted incinerators powered by generators provide a practical, adaptable solution for treating workers’ domestic waste, plastic containers, and oil-contaminated materials.
Rather than relying on long-distance waste transport or informal disposal methods, railway operators can evaluate mobile incineration as part of a structured environmental management approach suited to desert rail infrastructure.
For technical specifications and configuration options related to mobile and trailer-mounted incinerators, visit:
https://www.hiclover.com/
2025-12-14/01:28:21
|
Incinerator Items/Model |
HICLOVER TS100(PLC)
|
|
Burn Rate (Average) |
100kg/hour |
|
Feed Capacity(Average) |
150kg/feeding |
|
Control Mode |
PLC Automatic |
|
Intelligent Sensor |
Continuously Feeding with Worker Protection |
|
High Temperature Retention(HTR) |
Yes (Adjustable) |
|
Intelligent Save Fuel Function |
Yes |
|
Primary Combustion Chamber |
1200Liters(1.2m3) |
|
Internal Dimensions |
120x100x100cm |
|
Secondary Chamber |
600L |
|
Smoke Filter Chamber |
Yes |
|
Feed Mode |
Manual |
|
Burner Type |
Italy Brand |
|
Temperature Monitor |
Yes |
|
Temperature Thermometer |
Corundum Probe Tube, 1400℃Rate. |
|
Temperature Protection |
Yes |
|
Automatic Cooling |
Yes |
|
Automatic False Alarm |
Yes |
|
Automatic Protection Operator(APO) |
Yes |
|
Time Setting |
Yes |
|
Progress Display Bar |
3.7 in” LCD Screen |
|
Oil Tank |
200L |
|
Chimney Type |
Stainless Steel 304 |
|
1st. Chamber Temperature |
800℃–1000℃ |
|
2nd. Chamber Temperature |
1000℃-1300℃ |
|
Residency Time |
2.0 Sec. |
|
Gross Weight |
7000kg |
|
External Dimensions |
270x170x190cm(Incinerator Main Body) |
|
Burner operation |
Automatic On/Off |
|
Dry Scrubber |
Optional |
|
Wet Scrubber |
Optional |
|
Top Loading Door |
Optional |
|
Asbestos Mercury Material |
None |
|
Heat Heart Technology(HHT) |
Optional |
|
Dual Fuel Type(Oil&Gas) |
Optional |
|
Dual Control Mode(Manual/Automatic) |
Optional |
|
Temperature Record |
Optional |
|
Enhanced Temperature Thermometer |
Optional |
|
Incinerator Operator PPE Kits |
Optional |
|
Backup Spare Parts Kits |
Optional |
|
Mobile Type |
Optional:Containerized/Trailer/Sledge Optional |
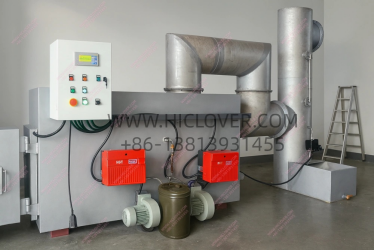
Ethiopia Waste Incinerator Market Report: Demand Characteristics, Local Trends, and Application of Modern Incineration Technologies
Ethiopia Waste Incinerator Market Report: Demand Characteristics, Local Trends, and Application of Modern Incineration Technologies
1. Overview of Ethiopia’s Waste Management Landscape
Ethiopia, with major cities such as Addis Ababa, Dire Dawa, and Mekelle, faces growing pressure to strengthen its municipal and medical waste treatment systems. Rapid population growth, expanding healthcare facilities, and industrial development have intensified waste generation, while landfill capacity and controlled disposal methods remain limited. Many regions continue to rely on open dumping or rudimentary burning, creating environmental and public-health challenges that local governments and international agencies seek to address urgently.
2. Key Market Characteristics
The waste incinerator market in Ethiopia shows several clear structural features:
-
High proportion of mixed municipal waste, often containing organic fractions that require stable combustion technologies.
-
Medical waste volumes increasing, especially in cities such as Hawassa and Bahir Dar, following hospital expansions and international health programs.
-
Remote regional clinics and field operations across Afar, Somali, and Oromia often lack centralized treatment, creating demand for mobile or containerized incineration systems.
-
Growing emphasis on emissions control, driven by both national environmental directives and the influence of global frameworks.
These characteristics create a market that values equipment reliability, flexible installation, and adaptable fuel options.
3. Demand Drivers and Market Trends
Several factors define the upward demand curve in Ethiopia:
-
Healthcare sector growth
Major hospitals in Addis Ababa and regional medical centers increasingly require compliant medical waste incinerators with multi-chamber designs and higher combustion efficiency. -
Expansion of humanitarian operations
Ethiopia frequently hosts programs supported by the United Nations, UNDP, WHO, and various NGOs operating in refugee camps, emergency shelters, and rural health units. These institutions often adopt standardized incineration solutions to meet safety and environmental requirements. -
Urbanization and population concentration
Cities such as Gondar and Adama generate large volumes of mixed waste, creating demand for medium-capacity units capable of continuous or semi-continuous operation. -
Shift toward regulated waste treatment
Ethiopia has been moving toward stricter oversight of medical and hazardous waste handling. This shift encourages adoption of engineered incinerators with secondary combustion chambers and optional wet scrubber systems.
4. Suitability of Incinerator Solutions to Ethiopia’s Local Conditions
Waste streams in Ethiopia are often high-moisture and inconsistently sorted. Suitable incineration systems therefore require:
-
High-temperature secondary combustion for complete burnout of low-calorific waste.
-
Diesel, LPG, or natural gas burners to stabilize combustion under variable moisture levels.
-
Top-loading or batch-loading chambers for bulky municipal refuse or community waste batches.
-
Mobile or containerized systems for deployment in remote regions where civil construction is limited.
These characteristics align well with solutions frequently deployed by UN field missions and health programs across East Africa.
5. HICLOVER Incinerators: Advantages for the Ethiopian Market
HICLOVER’s portfolio presents several strengths that match the requirements emerging in Ethiopia:
-
Top-loading and medical waste models optimized for hospitals in cities like Addis Ababa and Hawassa.
-
Containerized mobile incinerators ideal for NGOs and UN agencies working in regions such as Gambella, Afar, and Somali.
-
Multiple combustion chambers ensuring cleaner emissions and higher destruction efficiency, suitable for both municipal and hazardous waste.
-
Optional wet scrubbers and dry filtration for projects demanding enhanced environmental compliance.
-
Fast deployment capability, especially valuable for emergency or humanitarian missions.
-
Proven field track record across Africa, including installations supported by international development institutions.
These advantages allow HICLOVER systems to adapt to Ethiopia’s diverse operating environments, from dense urban districts to isolated rural clinics.
6. Additional Highlight: The Importance of Waste Treatment in Drought-Affected Zones
As Ethiopia continues to experience climate-driven pressures―including droughts in Somali, Afar, and parts of Oromia―the management of medical and community waste becomes increasingly critical. Limited water resources often restrict sanitary burial or controlled landfill operations. In such regions, compact and fuel-efficient incinerators provide a stable method for destroying infectious waste without relying on large civil infrastructure. This theme resonates strongly with humanitarian organizations overseeing emergency health operations.
7. Market Outlook
The Ethiopian waste incinerator market is expected to grow steadily due to:
-
Expansion of regional hospitals
-
Urban waste reforms in Addis Ababa and major secondary cities
-
International development projects requiring compliant waste treatment
-
Strengthened involvement of the United Nations, African Union mission facilities, and cross-border refugee-support programs
-
Rising emphasis on sustainability and emissions awareness
This combination of technical need, regulatory evolution, and institutional investment positions Ethiopia as one of the most dynamic incinerator markets in East Africa.
Ethiopia’s evolving waste management environment―shaped by healthcare expansion, population growth, and international humanitarian operations―creates strong demand for reliable waste incineration solutions. HICLOVER’s engineered systems, particularly their mobile, containerized, and medical waste units, align directly with local requirements across Addis Ababa, Mekelle, Dire Dawa, and remote operational zones.
Their robustness, adaptability, and compatibility with UN and NGO field standards position them as suitable solutions for Ethiopia’s long-term waste treatment strategy.
2025-12-11/14:01:00
|
Incinerator Items/Model |
HICLOVER TS100(PLC)
|
|
Burn Rate (Average) |
100kg/hour |
|
Feed Capacity(Average) |
150kg/feeding |
|
Control Mode |
PLC Automatic |
|
Intelligent Sensor |
Continuously Feeding with Worker Protection |
|
High Temperature Retention(HTR) |
Yes (Adjustable) |
|
Intelligent Save Fuel Function |
Yes |
|
Primary Combustion Chamber |
1200Liters(1.2m3) |
|
Internal Dimensions |
120x100x100cm |
|
Secondary Chamber |
600L |
|
Smoke Filter Chamber |
Yes |
|
Feed Mode |
Manual |
|
Burner Type |
Italy Brand |
|
Temperature Monitor |
Yes |
|
Temperature Thermometer |
Corundum Probe Tube, 1400℃Rate. |
|
Temperature Protection |
Yes |
|
Automatic Cooling |
Yes |
|
Automatic False Alarm |
Yes |
|
Automatic Protection Operator(APO) |
Yes |
|
Time Setting |
Yes |
|
Progress Display Bar |
3.7 in” LCD Screen |
|
Oil Tank |
200L |
|
Chimney Type |
Stainless Steel 304 |
|
1st. Chamber Temperature |
800℃–1000℃ |
|
2nd. Chamber Temperature |
1000℃-1300℃ |
|
Residency Time |
2.0 Sec. |
|
Gross Weight |
7000kg |
|
External Dimensions |
270x170x190cm(Incinerator Main Body) |
|
Burner operation |
Automatic On/Off |
|
Dry Scrubber |
Optional |
|
Wet Scrubber |
Optional |
|
Top Loading Door |
Optional |
|
Asbestos Mercury Material |
None |
|
Heat Heart Technology(HHT) |
Optional |
|
Dual Fuel Type(Oil&Gas) |
Optional |
|
Dual Control Mode(Manual/Automatic) |
Optional |
|
Temperature Record |
Optional |
|
Enhanced Temperature Thermometer |
Optional |
|
Incinerator Operator PPE Kits |
Optional |
|
Backup Spare Parts Kits |
Optional |
|
Mobile Type |
Optional:Containerized/Trailer/Sledge Optional |